DECENTRALISED WASTEWATER Treatment Sysyem
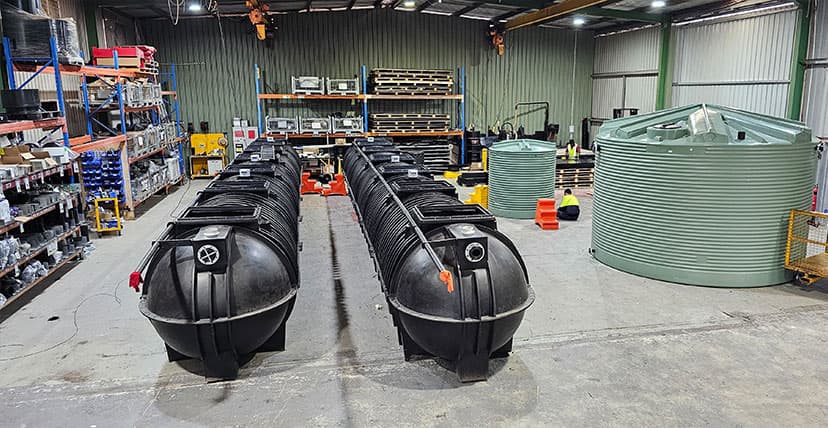
Working through head contractor Grounded Construction Group, Coerco engineered, manufactured, factory tested, delivered and commissioned complete decentralised water and wastewater solution for the MGM Lodge accommodation village in Port Hedland. The integrated package included 150 kL of insulated potable water storage (3 × 50 kL WaterMark-certified tanks), a pressure booster system with filtration and UV disinfection, a 4,000 L grease arrestor, two sewage pump stations across the village footprint, and a 40 kL/day MBBR wastewater treatment plant incorporating a 50 kL balance tank and 19 kL treated-effluent tank. Treated effluent is discharged to a multi-port flat-bed leach drain field for on-site disposal. The system was commissioned in October 2025.
THE CHALLENGE
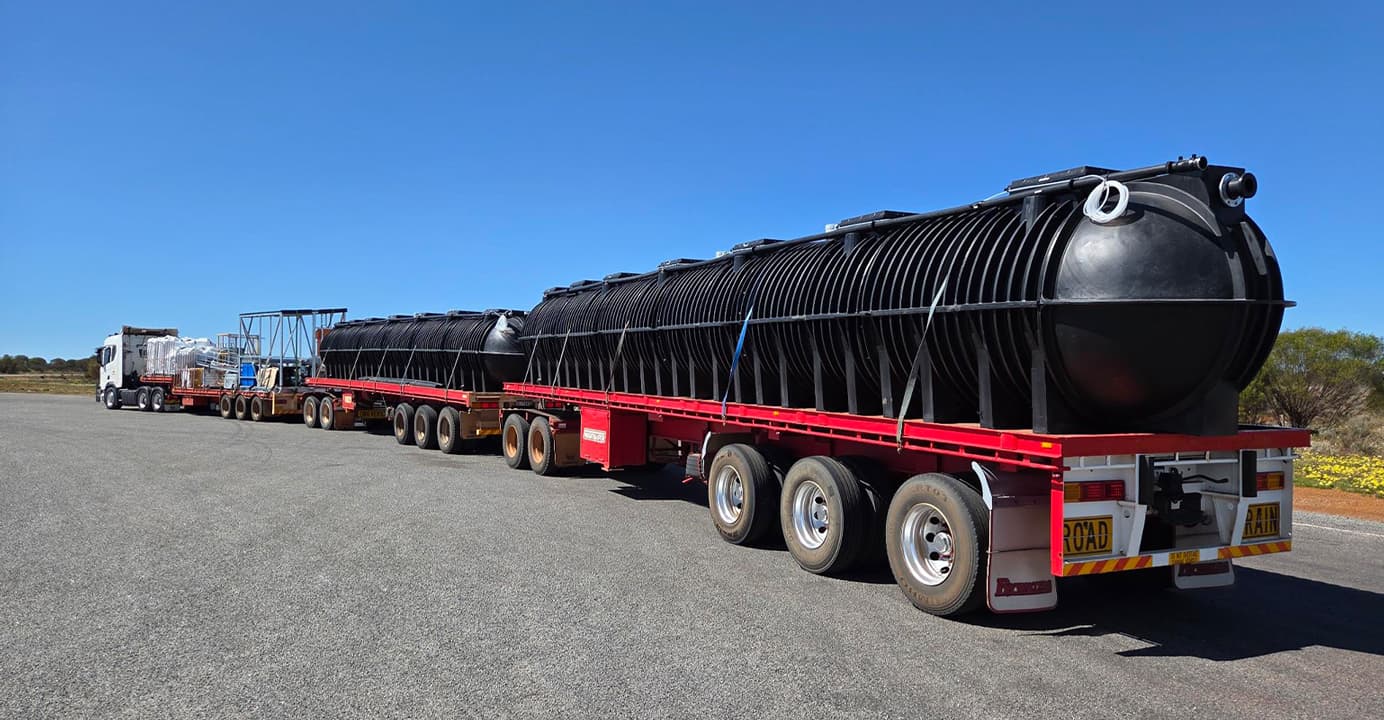
A remote workforce community with no access to conventional sewerage infrastructure, so all wastewater had to be collected, treated and on-site disposal.
The remote Pilbara site had high groundwater, so tanks were engineered for water-tightness in water-charged ground, with anti-flotation measures to keep groundwater out and the tanks in place.
Port Hedland sits in a cyclonic wind region (Region D), so the system was engineered for cyclonic wind loads in accordance with AS/NZS 1170.2, including cyclonic tie-downs.
THE SOLUTION
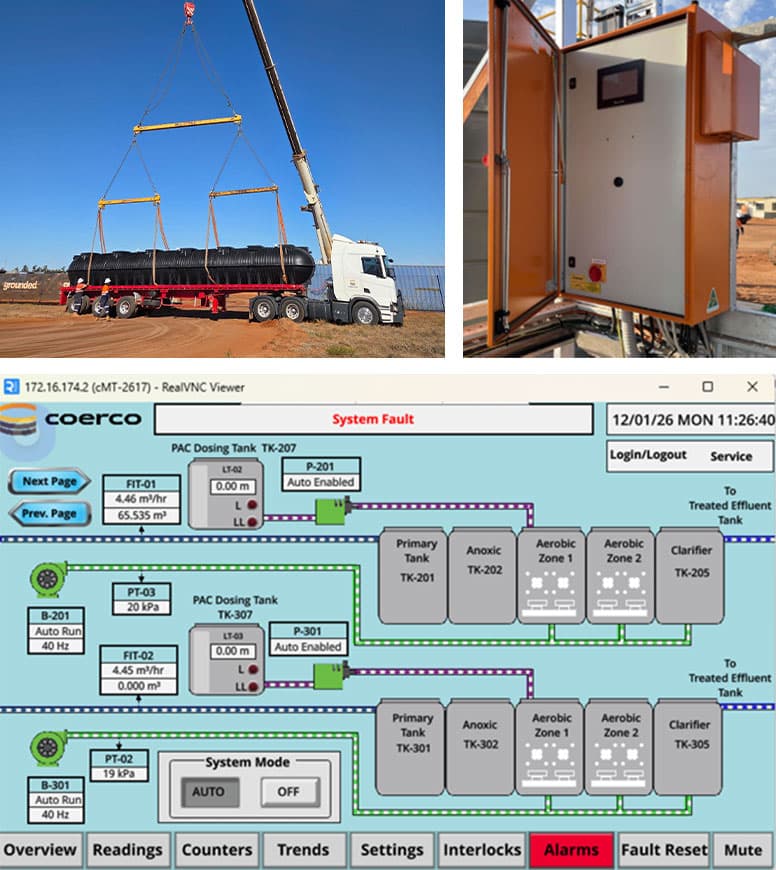
Wastewater generated across the village is collected via two sewage pump stations, each equipped with duty/standby grinder pumps, automatic dual-pump control and high-level alarms. Wastewater from the kitchen facilities is separately pre-treated through a Coerco 4,000 L grease arrestor to remove fats, oils and grease before entering the main wastewater collection system. An automatic inlet screening removes coarse solids and other debris, protecting downstream pumps and treatment equipment.
Screened wastewater is received in a 50 kL balance tank, providing equalisation of the variable hydraulic and organic loads generated across the village. The balance tank buffers peak flows and variations in wastewater strength, while controlled pumping delivers wastewater to the biological treatment trains at a regulated flow rate. This provides more consistent hydraulic and organic loading to the biological process, reducing peak loading impacts and supporting stable biological treatment and reliable plant performance.
The wastewater treatment plant has a design capacity of 40 kL/day (40 m³/day) and comprises two parallel 20 kL/day treatment trains. Each train incorporates primary treatment, an anoxic fixed-film biological treatment and two aerobic Moving Bed Biofilm Reactor (MBBR) stages, followed by secondary clarification. The staged biological process provides organic matter removal and biological nitrogen reduction, with the anoxic zone supporting denitrification. Polyaluminium chloride (PAC) dosing provides additional phosphorus control. Following clarification, treated effluent is disinfected by chlorination and transferred to a 19 kL treated-effluent storage tank equipped with dual discharge pumps. The plant incorporates automated process control together with remote monitoring and control capabilities, enabling key operating parameters, equipment status and alarms to be monitored remotely.
WHY CHOOSE US

As a family-owned business, we're passionate about improving lives, supporting charitable causes, and actively participating in community events while creating local jobs.

We provide exceptional customer care with prompt, efficient, tailored solutions, actively listening to your feedback and offering genuine support from first contact through post-delivery.

Our 30+ years of in-house engineering expertise and 150+ skilled team deliver innovative solutions using the widest product range and strategic industry partnerships.
Years In Business
Team Members
Square Metres of Manufacturing
